WBP plywood归档 - NQ Formwork Plywood Co., Ltd.

For international civil engineering contractors, receiving substandard formwork plywood on jobsites leads to serious structural failures: wall bulging, joint blowout, surface spalling, and panel delamination during concrete pouring. Because low-grade panels can look similar on the surface, buyers must understand practical inspection methods to verify panel quality.
Understanding these essential quality benchmarks protects your budget and helps you distinguish long-lasting architectural panels from low-grade alternatives.
1. Differentiating Fresh Hardwood Cores from Recycled Scrap Boards
The internal timber structure determines a panel’s load-bearing capacity and screw withdrawal resistance.
-
Grade-A Eucalyptus & Pine Core (High Structural Strength): High-quality panels utilize fresh, whole rotary-cut eucalyptus veneers paired with tough pine faces. The dense cellular grain provides high static bending strength, resisting the hydrostatic head pressure of fresh concrete without internal cracking.
-
Finger-Joint Recycled Core (High Failure Hazard): Low-cost suppliers often sell finger-joint panels made from fragmented timber off-cuts glued together with cheap urea adhesives. These boards contain hidden internal hollows and discontinuous grain fibers. Under concrete pressure or vibration, they often crush, cave in, or snap after only 1 to 2 pours.
2. Identifying True 100% WBP Phenolic Waterproof Glue
The adhesive line between plies determines whether formwork will withstand wet concrete hydration and heavy rains.
-
The 72-Hour Continuous Boil Test: Authentic Water Boiled Proof (WBP) phenolic adhesive undergoes an irreversible cross-linking reaction during hot pressing. When a sample board is boiled in continuous 100 degrees Celsius water for 72 hours, it remains solid with zero blister swelling or ply separation.
-
The Limitation of Urea and Low-Melamine Glues: Low-grade urea-formaldehyde glue melts in hot water within 1 to 2 hours. While melamine offers moderate water resistance, continuous exposure to hot, alkaline slurry eventually breaks its molecular bonds, causing the board to swell and soften on the jobsite.
3. Practical On-Site Verification Steps
Before signing off on full container shipments, site supervisors can verify panel quality using four simple steps:
-
Cross-Section Saw Inspection: Cut off a 100mm section from the board corner. A quality panel shows solid, tightly bonded veneers with dark resin glue lines, showing zero hollow pockets or overlapping voids.
-
Caliper Thickness Measurement: Use a digital vernier caliper to check thickness consistency across all four edges and corners. High-precision boards maintain tight tolerances within +/- 0.5mm, preventing step-joints and slurry leakage during site assembly.
-
Surface Film Scratch & Peel Test: High-density 150g/㎡ phenolic paper forms a smooth, hard surface that resists fingernail scratches and prevents peeling from the core veneers.
-
Chisel Fracture Check: Drive a wood chisel between the wood plies of a boiled test piece. In a certified hardwood board, the wood fibers tear internally before the glue line separates, proving the adhesive bond is stronger than the wood itself.
For projects requiring high-cycle fair-face finishes, contractors specify 18mm heavy-duty film-faced plywood manufactured by NQ Formwork Plywood Co., Ltd. to achieve 15 to 20 reliable cycles. Standard floor framing relies on 12mm red formwork boards for 6 to 8 dependable cycles.
To view live laboratory boiling shear tests and computerized sanding operations, watch our factory production video stream, study our corporate manufacturing overview, or contact our technical export specialists.
-
Official Website: https://nqformwork.com/
-
Direct WhatsApp: +86 19977575391
Selecting between black film faced plywood and red phenolic formwork boards is one of the most critical decisions in civil engineering procurement. While both panel types provide structural support for poured concrete, their surface treatments, demolding finishes, and expected life cycles serve distinct construction needs.
Understanding the differences between these two plywood types prevents overspending on secondary residential frames while eliminating surface defects on architectural fair-face concrete.
Surface Characteristics and Concrete Texture
The primary difference between film faced plywood and red formwork boards lies in the surface barrier and how it interacts with wet concrete:
-
Black Film Faced Plywood: Hot-pressed with high-density phenolic resin-impregnated paper (120g/m2), this panel creates a sealed, non-porous polymer barrier. Cured concrete demolds with a smooth, glass-like finish known as fair-face concrete. Because the surface is free of cement dust and wood grain marks, it eliminates the need for plastering, saving labor and material costs.
-
Red Phenolic Formwork Board: Coated on both sides with acrylic-modified phenolic waterproof paint, red panels protect the inner timber veneers from rain and wet cement paste. Demolded concrete retains a subtle wood texture, providing excellent mechanical bonding for secondary cement mortar rendering and tile installations.
Core Construction and Structural Durability
Beneath the surface, both panels manufactured by NQ Formwork Plywood Co., Ltd. utilize 100% Grade-A pine and eucalyptus combi cores bonded with 100% WBP phenolic adhesive.
-
Film Faced Plywood (High-Rise & Columns): The polymer film protects the timber plies against abrasive cement paste and alkaline leaching. This durable surface barrier allows heavy structural panels (such as 18mm boards) to achieve 15 to 20 reuse cycles under high lateral concrete pressures.
-
Red Formwork Boards (Floor Slabs & Beams): Designed for horizontal applications where structural panels face less abrasive pumping friction, standard red panels deliver dependable performance across 6 to 15 pours, depending on whether 12mm or heavier thicknesses are deployed.
Strategic Board Allocation on the Jobsite
To optimize procurement costs, experienced project managers deploy a hybrid panel strategy across structural zones:
-
Vertical Shear Walls & Elevator Cores: Use black film faced plywood. The high-gloss phenolic face resists lateral slurry friction, ensuring smooth surfaces across repeated pours.
-
Horizontal Floor Decks & Foundation Slabs: Use red phenolic formwork boards. These panels provide necessary load-bearing stiffness at a lower procurement cost, ideal for flat slabs that will receive ceiling finishes or flooring later.
To compare physical sample textures, inspect surface coatings, and review production standards, watch our factory testing video stream, study our corporate manufacturing overview, or contact our export engineering specialists.
-
Official Website: https://nqformwork.com/
-
Direct WhatsApp: +86 19977575391
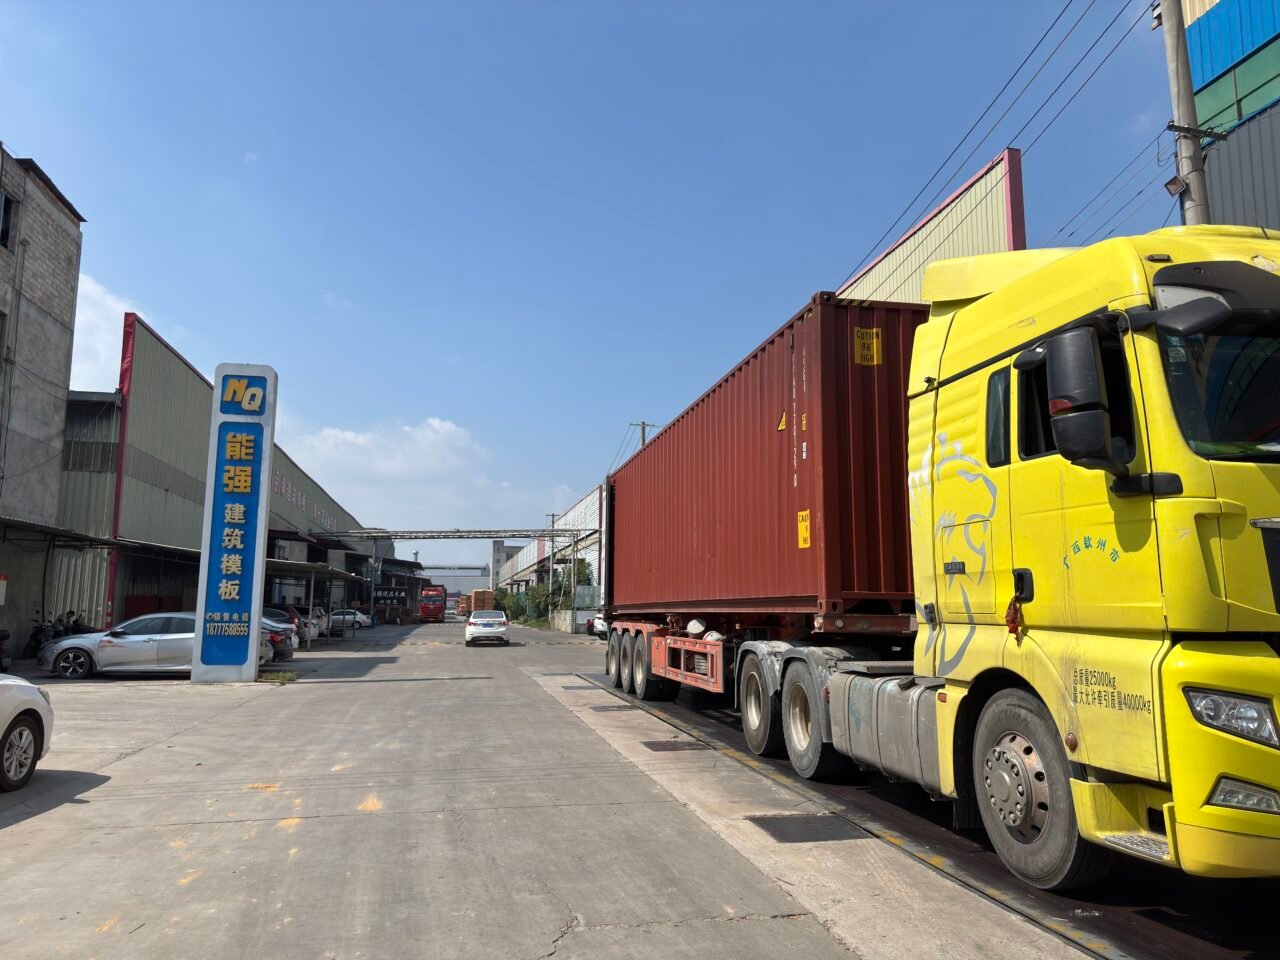
In the global building materials market, securing a dependable, large-scale source of shuttering panels is critical for high-rise commercial contractors and building material distributors. Project delays, joint slurry leakage, and uneven concrete finishes frequently trace back to small, inconsistent suppliers unable to maintain quality standards across large batches.
Guangxi, China is recognized as the world’s leading industrial base for pine and eucalyptus timber production. Within this timber manufacturing cluster, NQ Formwork Plywood Co., Ltd. operates as an established primary producer, providing global construction projects with durable architectural formwork solutions direct from the mill.
Modern Manufacturing Scale and Infrastructure
Operating expansive workshop facilities in Batang Industrial Park, Guangxi, our production base maintains an annual manufacturing capacity exceeding 5,000,000 sheets, with over 1,000,000 sheets exported annually to commercial infrastructure projects worldwide.
The manufacturing facility integrates modern automated production lines:
-
Automated Continuous Veneer Peeling & Sorting: Fresh eucalyptus logs are rotary-peeled into solid whole veneers, eliminating decayed pieces, bark pockets, and irregular grain before panel assembly.
-
Multi-Roller Glue Coating: Automated adhesive spreaders guarantee full, uniform resin penetration across every single layer, preventing dry spots and unglued seams.
-
High-Tonnage Multi-Cylinder Hydraulic Hot Pressing: Panels undergo prolonged hydraulic heat and compression, curing the adhesive into an irreversible cross-linked bond resistant to water, heat, and concrete pressure.
-
Computerized CNC Edge Trimming: High-precision double-end tenoners mill all four edges to strict right angles, ensuring flush panel joints on jobsites.
Primary Product Lines for Commercial Engineering
The factory specializes in two core categories of concrete formwork:
-
Black Film Faced Plywood (Fair-Face Shuttering): Engineered with 100% Grade-A pine and eucalyptus combi cores and hot-pressed with high-density phenolic surface film. It delivers glass-smooth, fair-face concrete finishes with a service life of 15 to 20 reuse cycles on vertical walls and columns.
-
Red Phenolic Formwork Plywood: Coated with waterproof acrylic-phenolic paint over dense hardwood cores. It provides a reliable, cost-effective framing solution for residential floor slabs and beam bottoms, delivering 6 to 15 reuse cycles.
Both product lines utilize in-house synthesized 100% WBP (Water Boiled Proof) phenolic glue, guaranteeing that panels will not delaminate even under severe rainy conditions or prolonged boiling water tests.
Streamlined Ocean Shipping Logistics
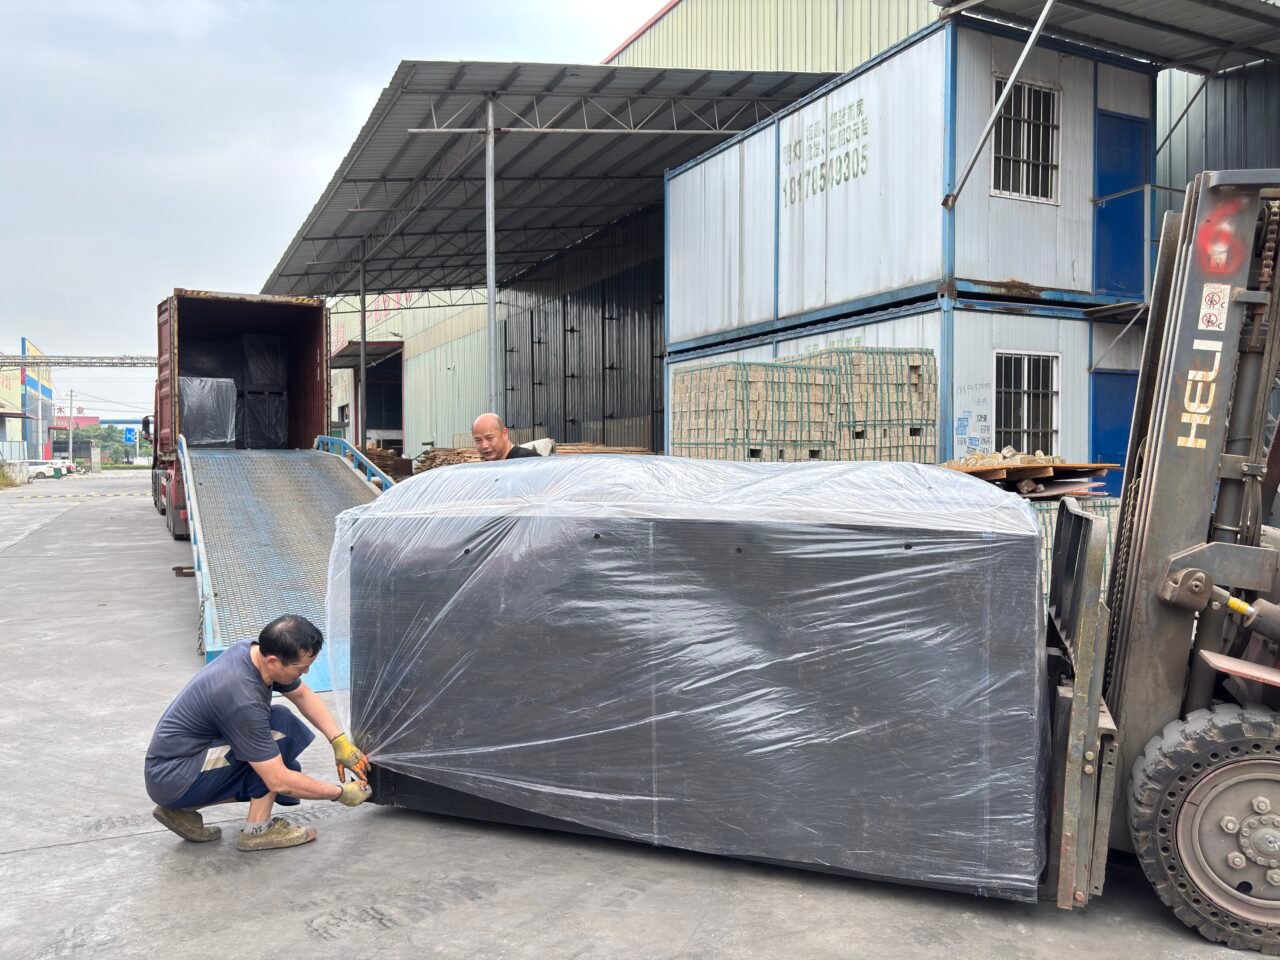
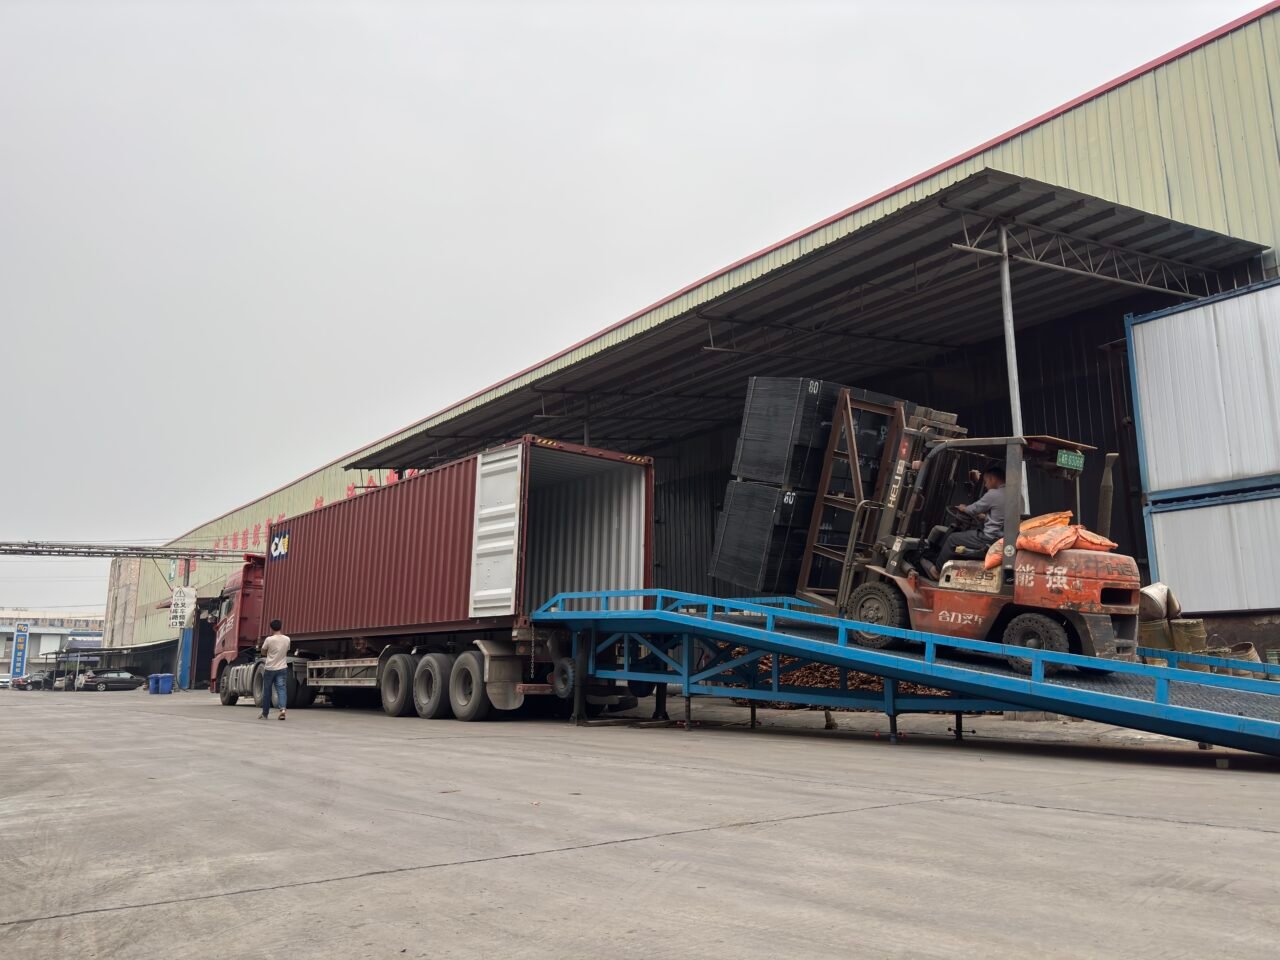
Located near major expressway networks with direct access to Qinzhou Port, the facility coordinates smooth container consolidation and rapid vessel dispatch. Standard export orders are ready for vessel loading within 7 to 15 days, providing global builders with consistent replenishment for tight construction schedules.
To explore our timber production lines, inspect veneer grading, and review technical testing, visit our factory live production stream, study our corporate manufacturing overview, or connect with our international export team.
-
Official Website: https://nqformwork.com/
-
Direct WhatsApp: +86 19977575391
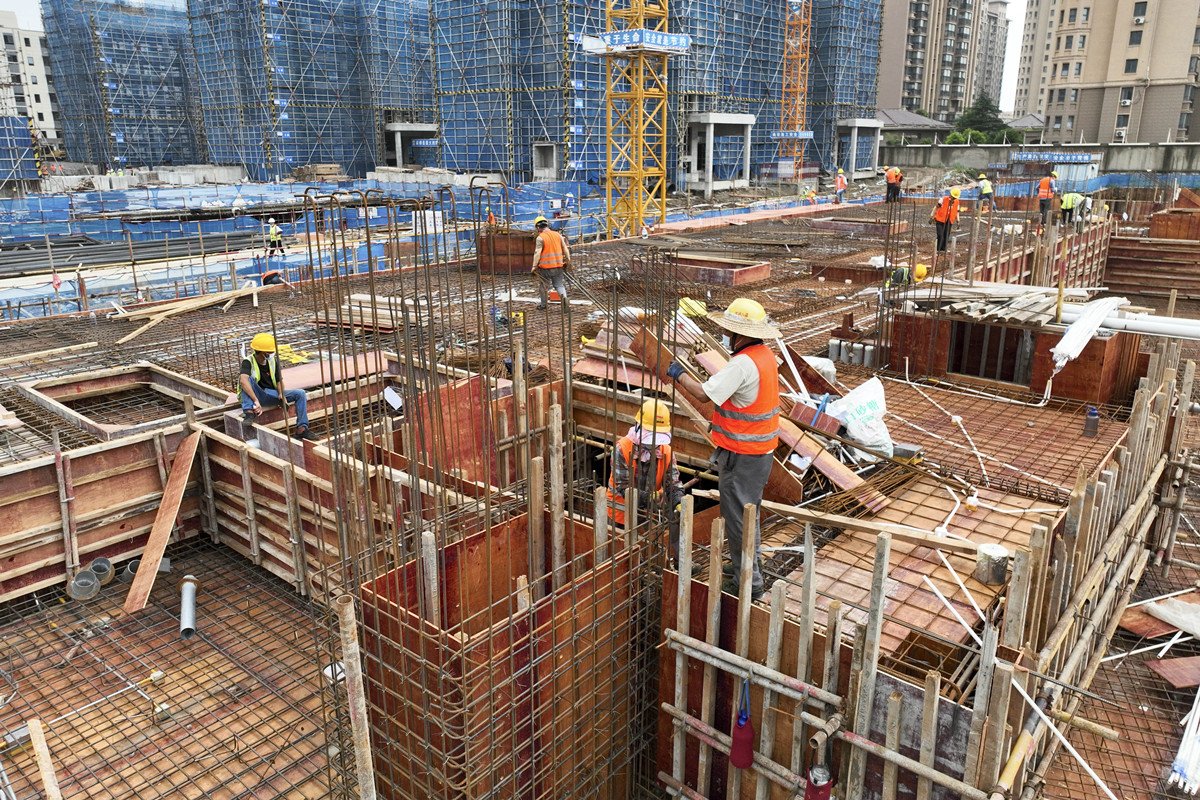
In commercial concrete construction, formwork accounts for a substantial portion of structural pacing and safety. Selecting substandard shuttering panels often leads to joint slurry leakage, surface bulging, premature delamination, and costly concrete chipping after striking.
With dozens of formwork plywood options circulating in the global market, civil engineering contractors and commercial procurement managers need clear benchmarks to distinguish high-performance panels from low-grade alternatives. Understanding core veneer species, adhesive bonding, and specification gradients is essential to securing reliable panels for jobsite pours.
1. Identifying the Core Material: Eucalyptus, Pine, Poplar, and Recycled Wood
The internal veneer composition dictates a panel’s load-bearing stiffness, screw-holding strength, and resistance to repeated hydrostatic head pressures.
-
Grade-A Eucalyptus & Pine Core (Heavy-Duty Engineering Standard): Fast-growing southern eucalyptus veneers possess high cellular density (580 to 640 kg/m3), delivering an exceptional modulus of elasticity and rupture. When combined with tough pine surface veneers in a cross-laminated structure, the board resists flexural cracking under high-pressure pumping, preventing wall bulging.
-
Northern Poplar Core (Lightweight Framing): Poplar wood is naturally softer and less dense (around 420 to 480 kg/m3). While lighter to handle on manual residential decks, standard poplar boards offer lower screw withdrawal resistance and higher deflection under heavy vertical wall pressures.
-
Recycled Finger-Joint Scrap Core (High Failure Risk): Manufactured from fragmented jobsite plywood off-cuts and secondary cold-press glue, finger-joint boards conceal internal air voids and lack continuous grain fibers. Under the hydraulic shock of fresh concrete, these panels frequently fracture or cave in after just 1 to 2 pours.
2. Film Faced Plywood vs. Red Phenolic Board: Matching the Surface to the Pour
Surface coatings define the final architectural texture of cured concrete and determine edge protection against wet cement alkalinity.
-
Black Film Faced Plywood (Shuttering Plywood): Hot-pressed with high-density phenolic resin-impregnated paper (120g/m2), this panel forms an impermeable shield against abrasive slurry. The cured concrete surface is mirror-smooth (fair-face concrete), eliminating the need for secondary wall plastering. It is ideal for bridge piers, high-rise shear walls, and elevator shafts requiring 8 to 20 reuse cycles.
-
Red Phenolic Formwork Board: Coated on both faces with an acrylic-phenolic waterproof resin paint, red panels protect raw veneers while leaving a subtle micro-texture on demolded concrete. This surface profile creates a natural bond for secondary cement mortar rendering and tile adhesives. For horizontal slab soffits and foundation beams requiring 6 to 15 reuses, red formwork provides high rigidity at lower procurement costs.
3. Four Practical On-Site Methods to Inspect Formwork Plywood Quality
Before signing off on full container shipments, site inspectors can verify board integrity using four straightforward tests:
-
Caliper & Thickness Tolerance Check: Measure all four edges and corners with a digital vernier caliper. Precision-milled architectural boards maintain thickness consistency within +/- 0.5mm across the entire 2440mm length, preventing step-joint gaps and slurry blowout during assembly.
-
Cross-Section Void Inspection: Cut a 100mm section off the panel corner. High-grade panels display tight, solid veneer plies bonded with dark resin lines, showing zero interior hollow cavities.
-
The 72-Hour Boiling Water Test (BWP Standard): Boil a sample piece in rolling 100 degrees Celsius water. Authentic panels bonded with 100% WBP (Water Boiled Proof) phenolic glue endure continuous boiling without blister swelling or glue release.
-
Single Sheet Weight Audit: Core density directly correlates with board mass. In standard 4×8 ft (2440x1220mm) panels, a genuine dense 18.0mm sheet weighs approximately ~34.48 kg, while a 12.0mm sheet weighs approximately ~23.26 kg. Panels weighing substantially less often indicate soft filler plies or hollow internal gaps.
4. Thickness Specifications & 40ft HQ Container Capacity Reference
Matching panel thickness to joist spacing optimizes site safety and ocean shipping efficiency. Commercial manufacturers engineer precise thickness tiers to respect maritime container payload limits of 26.0 to 28.5 metric tons:
| Thickness Tier JPG | Single Sheet Weight JPG | Packaging Bundle JPG | 40ft HQ Load Capacity JPG | Expected Reuse Pours JPG |
| 12.0 mm Panel |
~23.26 kg |
100 Sheets / Pack |
~1,208 Sheets
|
8-12 (Film) / 6-8 (Red) |
| 14.0 mm Panel |
~27.03 kg |
85 Sheets / Pack |
~1,036 Sheets
|
12-15 (Film) / 8-10 (Red) |
| 16.0 mm Panel |
~30.77 kg |
60 Sheets / Pack |
~906 Sheets
|
13-17 (Film) / 10-12 (Red) |
| 18.0 mm Panel |
~34.48 kg |
60-70 Sheets / Pack |
~805 Sheets
|
15-20 (Film) / 12-15 (Red) |
For projects requiring heavy vertical pours and fair-face architectural finishes, contractors deploy 18mm heavy-duty film-faced plywood manufactured by NQ Formwork Plywood Co., Ltd. to achieve 15 to 20 cycles. For standard floor slab decks, 12mm red formwork boards maximize container volume and support dependable 6 to 8 cycles.
To view veneer rotary peeling, automated hot press lines, and container loading operations, watch our factory production video stream, study the company manufacturing overview, or request structural product specifications.
-
Official Website: https://nqformwork.com/
-
Direct WhatsApp: +86 19977575391

Our products include:
Plywood Formwork, Film Faced Plywood, Clean Water Formwork, Concrete Formwork Panels, PP Plastic Coated Plywood, Red/Black Film Plywood, Bridge Formwork, and Construction Panels.
Standard sizes: 1830×915mm, 2440×1220mm, 1830×1220mm
Thickness: 10–20mm (customized available)
Surface glue uses phenolic glue, and core glue is self-produced, ensuring better waterproofing and bonding strength.
Daily output reaches 30,000 sheets. We export widely to Southeast Asia including the Philippines, Vietnam, Malaysia, Indonesia and Cambodia.