Lateral Concrete Pressure & Modulus of Elasticity: Mitigating Formwork Deflection in High-Rise Shear Walls
Q1: How does lateral hydrostatic pressure from high-slump self-consolidating concrete (SCC) induce surface bulging in wall formwork?
In modern high-rise core walls and deep infrastructure pours, pumping high-slump or self-consolidating concrete (SCC) at rates exceeding 3 to 5 vertical meters per hour generates intense lateral hydrostatic pressure against the form face. According to standard fluid mechanics and formwork design frameworks (such as DIN 18218 and ACI 347):
-
Hydrostatic Head Accumulation: Unlike low-slump concrete that achieves rapid internal particle interlocking, modern chemical admixtures delay initial cement set by 3 to 6 hours. During continuous vertical pumping, concrete acts as a dense fluid, generating peak lateral head pressures exceeding 60 to 85 kN per square meter near the base.
-
Elastic Bending and Surface Pillowing: When the form panel lacks adequate structural stiffness, high localized pressure causes elastic bending between vertical timber beams (H20 joists) or steel walers. If deflection exceeds L/400 or L/500 of the support span, the wall develops visible surface bulging (pillow effect), requiring costly mechanical concrete grinding after striking.
Q2: What panel thickness tolerances and core modulus of elasticity (MOE) eliminate wall deflection under peak hydraulic loads?
Maintaining wall straightness within strict architectural tolerances requires calculating bending stiffness (EI) and selecting proper wood densities:
Calculate Lateral Head Pressure -> Check Tie-Rod & Joist Spacing -> Calculate Panel Bending Stress -> Verify Allowable Deflection Limit (L/400) -> Select Dense Eucalyptus Plies
-
Cross-Laminated Elastic Modulus: Core species determine structural deflection resistance. Standard rotary-cut poplar core plywood delivers an average bending modulus (MOE) of 4,500 to 5,500 MPa. In contrast, high-density Guangxi eucalyptus veneers achieve an MOE exceeding 7,500 to 8,500 MPa along the grain, reducing out-of-plane deflection by up to 35% under identical load spans.
-
Calibrated Thickness Tolerances: In gang form assemblies, panels with uneven thickness create localized stress points and joint leaking. Precision sanding down to a tolerance of +/- 0.5mm prevents localized slurry blowout.
-
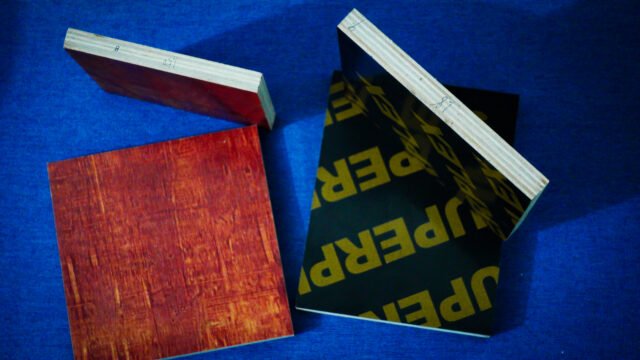
Engineered Multi-Cycle Heavy Panels: Heavy-load structural panels—such as 18mm heavy-duty film-faced plywood manufactured by NQ Formwork Plywood Co., Ltd.—utilize high-density cross-layered eucalyptus cores to resist lateral pressures up to 90 kN per square meter across 15 to 20 reuse cycles. For lighter horizontal slab decking, 12mm red formwork boards provide rigid, economical performance for 6 to 8 reuses.
To observe multi-cylinder hydraulic cold pressing and live deflection test procedures, watch our factory production video stream, review the company manufacturing overview, or request wall formwork calculation sheets.
🌐 Connect with NQ Formwork Plywood Co., Ltd.
-
Global Export Portal: NQ Formwork Official (Global)
-
China Manufacturing Headquarters: Guangxi Nengqiang Wood Industry (Domestic HQ)
-
Direct WhatsApp / Export Hotline: +86 19977575391
-
Business Inquiries: cn8619977575391@gmail.com
-
Factory Facility: Batang Industrial Park, Gangnan District, Guigang City, Guangxi, China