Working hours:Mon - Fri 9.00 - 18.00 Call Us: (+86) 19977575391

购物车

GET A QUOTE

Papan Kayu Plywood归档 - 第5页 共9页 - NQ Formwork Plywood Co., Ltd.

c6b9daa6ced87b6ad5044ec562bbc35e.jpeg

2026-09-090

Q1: What is the mechanical difference between 120g/m² and 240g/m² phenolic overlays on concrete formwork?

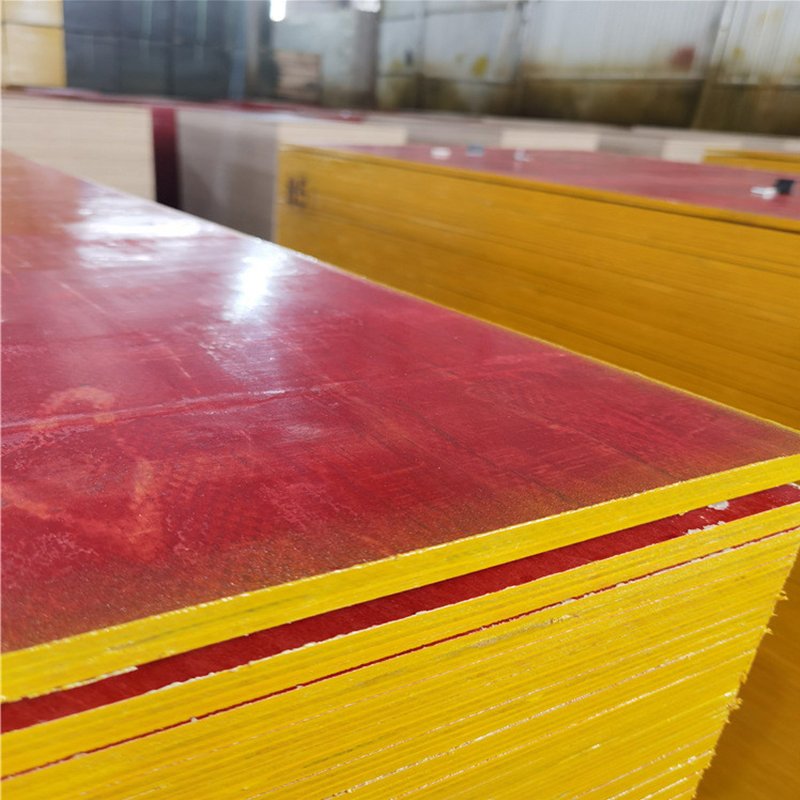
The outer protective layer on high-grade film-faced plywood is an engineered Kraft paper impregnated with thermosetting phenolic resin. Film thickness and resin content are universally classified by basis paper weight: 120g/m² and 240g/m² (or double-layer treated papers).

Material Science Differences
  1. Resin Saturation Index: A 120g/m² film carries roughly 60–70 grams of cured phenolic resin per square meter, forming a 0.12mm waterproof film. A 240g/m² heavy-duty film carries over 130 grams of cured resin, creating an impenetrable polymer barrier over 0.22mm thick.

  2. Taber Abrasion Resistance: Under standardized ASTM Taber abrasive testing (CS-17 wheels, 1,000g load):

    • 120g/m² standard film sustains 350 to 500 abrasion cycles before wood fibers show through.

    • 240g/m² heavy-duty film sustains 800 to 1,200 abrasion cycles, providing superior endurance against aggregate scraping during high-slump concrete vibrations.

Q2: How do civil contractors match film specifications to specific concrete finish requirements?

Matching overlay weight to project parameters prevents overspending on secondary plastering:

Overlay Engineering Application Matrix
Project Requirement Recommended Film Grade Core Configuration Reusability Horizon
Standard Residential Slabs Resin Paint / 120g/m² Film 12mm Red Board 6 – 8 Reuses
Commercial Fair-Face Concrete 120g/m² Phenolic Overlay 15mm–18mm Eucalyptus 10 – 12 Reuses
High-Rise Core Walls & Piers 240g/m² Heavy Phenolic 18mm Heavy-Duty Plywood 15 – 20 Reuses
Bridge Abutments & Dams 240g/m² Double-Coated 20mm Custom Engineered 15 – 20 Reuses

For civil engineering contractors across Dubai, Saudi Arabia, and the Philippines, utilizing 240g/m² overlays on 18mm heavy-duty panels manufactured by NQ Formwork Plywood Co., Ltd. eliminates concrete slurry water absorption. This guarantees a mirror-smooth architectural concrete surface that requires zero secondary cement skimming or plastering.

Review daily film hot-pressing quality controls by watching our factory live production videos, browse our complete formwork catalog, or request direct factory container pricing.

🌐 Connect with NQ Formwork Plywood Co., Ltd.


050.jpg

2026-09-080

Q1: Why do formwork panels fail around tie-rod sleeves and perimeter clamps during continuous climbing pours?

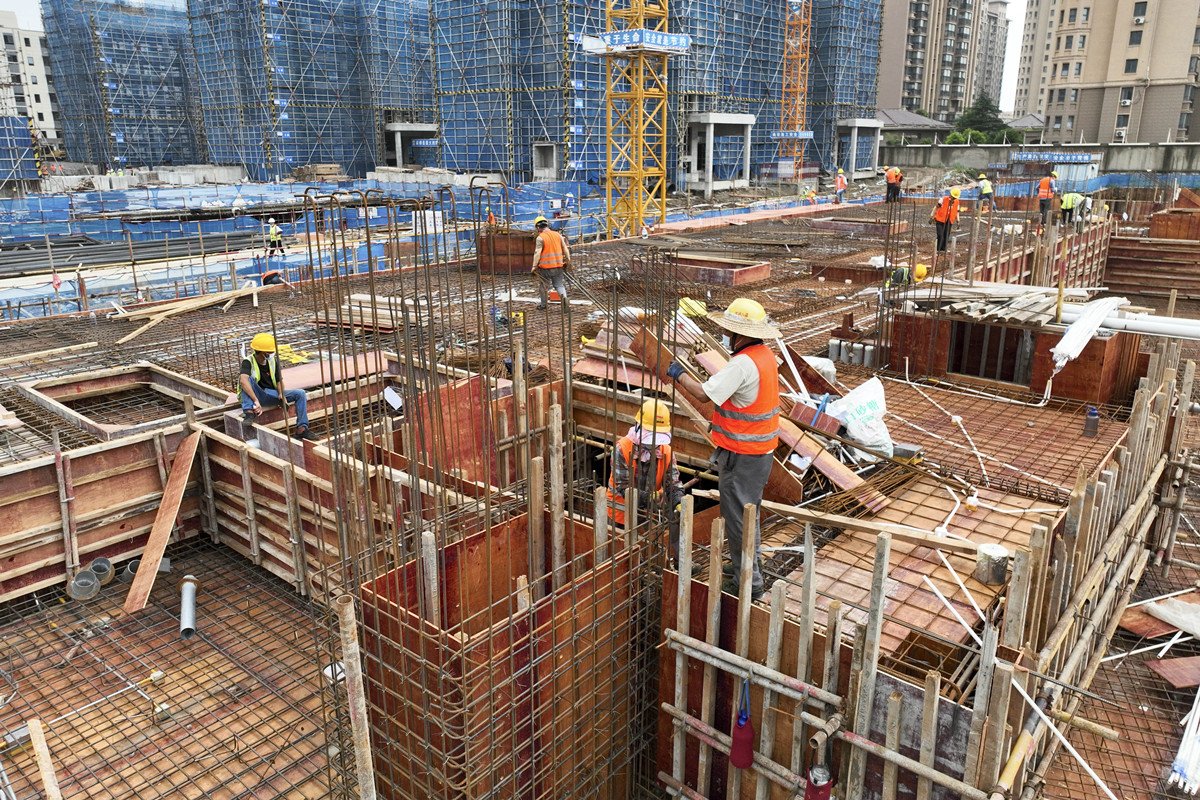
In self-climbing formwork (SCF) and crane-lifted gang forms used across high-rise towers in Dubai, Riyadh, and Doha, formwork panels experience severe concentrated mechanical shear around tie-bolt holes and perimeter steel frame clamps. When fresh concrete is placed, tension along through-tie rods can reach 40 to 90 kN depending on wall thickness and pour rate.

Panel failure in these zones typically occurs through two mechanisms:

  1. Localized Bearing Crushing: Low-density core veneers (such as light poplar or uncompressed mixed woods) have low perpendicular-to-grain compressive strength. The washer plate or clamp crushes into the outer plies, puncturing the phenolic film and allowing water ingress.

  2. Screw Strip-Out (Withdrawal Failure): During stripping and lifting cycles, wind vibrations and crane lifting forces exert cyclic pulling loads on the countersunk screws securing the plywood to the steel framing. Low-density veneers strip their wood threads easily, causing perimeter detachment.

Q2: How does core density determine fastener retention and edge durability in heavy-duty formwork?

Screw holding capacity is directly proportional to wood density squared. Engineering high-load climbing systems requires specific wood species and cross-ply configurations:

Fastener Mechanical Performance by Core Type
Mechanical Parameter Poplar Core (Low Density) Southern Mixed Hardwood Dense Eucalyptus Multi-Ply
Average Density 430–480 kg/m³ 520–580 kg/m³ 620–680 kg/m³
Face Screw Withdrawal ~1,100 N ~1,450 N > 1,950 N
Edge Screw Withdrawal ~850 N ~1,100 N > 1,500 N
Tie-Hole Bearing Strength Moderate / Prone to Crushing High Superior Shear Resistance

By using full-sheet Southern Eucalyptus veneers bonded under high-pressure thermal cycles, structural panels—such as 18mm heavy-duty film-faced plywood manufactured by NQ Formwork Plywood Co., Ltd.—resist perimeter screw strip-out and provide 15 to 20 reuse cycles in climbing systems without hole elongation. For lower-load horizontal applications, 12mm red formwork boards offer an economical 6 to 8 reuses.

To observe factory tie-rod hole drilling tolerances and panel strength tests, access the factory daily video library, review the company background, or consult export structural specialists.

🌐 Connect with NQ Formwork Plywood Co., Ltd.

default

DSC04324-1280x720.jpg

2026-09-070

Q1: How does uneven veneer moisture content cause internal steam blistering during high-temperature hot pressing?

In industrial plywood manufacturing, veneer moisture control is the single most critical variable determining internal bond strength. When raw eucalyptus logs are rotary-peeled into 1.5mm–2.2mm veneers, natural green moisture levels often exceed 40% to 60%. If veneers are insufficiently dried before assembly—or if ambient humidity introduces uneven moisture pockets—moisture content will exceed the safe threshold of 8% to 12%.

During the hydraulic hot-pressing phase, steel platens apply continuous heat (125℃ to 140℃) under pressures exceeding 2.0 to 2.5 MPa to cure the phenolic resin. If core veneers retain excessive moisture, this water instantly vaporizes into high-pressure steam trapped within the tight wood plies. Because phenolic resin requires moisture-free conditions to complete cross-linked polycondensation, the localized steam pressure dilutes the resin solids and physically blows apart the adhesive layer. When the press decompresses, these steam pockets expand rapidly, creating internal blisters, unbonded voids, and latent delamination zones that are invisible from the outside but fail under the first concrete pour.

Q2: What drying and pressing protocols ensure maximum structural bonding in commercial shuttering boards?

Leading industrial manufacturers in regional timber clusters eliminate steam blistering through continuous automated drying and calibrated multi-stage pressure release:

Roller Jet Drying (<10% Moisture) ➔ Double-Sided Resin Roll-Coating ➔ Cold Pre-Press ➔ High-Pressure Hot Pressing ➔ Gradual Decompression
  1. Continuous Roller Jet Drying: Veneers pass through multi-deck roller dryers with circulating hot air, reducing moisture variance to within ± 1.5\% across every sheet.

  2. Gradual Decompression Cycles: Hydraulic presses utilize micro-stepped pressure reduction cycles during the final 30 seconds of pressing, allowing residual microscopic steam to vent safely before platens open.

  3. Optimized Structural Durability: Controlling internal moisture ensures that structural panels—including 12mm red formwork boards (rated for 6–8 reuses) and heavy-duty 18mm film-faced plywood (delivering 15–20 reuses) produced by NQ Formwork Plywood Co., Ltd.—maintain shear bond strength exceeding 1.2 MPa under severe boiling water tests.

To examine industrial roller drying and press line operations, review the NQ factory video stream, study the corporate manufacturing overview, or request structural plywood technical data.

🌐 Connect with NQ Formwork Plywood Co., Ltd.


敲板区1-1-拷贝-1280x720.jpg

2026-09-040

Q1:What chemical reactions occur between wet alkaline concrete and shuttering adhesives under 45°C+ Middle Eastern desert temperatures?

Fresh concrete paste is a harsh chemical environment with a pH between 12.5 and 13.5, driven by calcium hydroxide ($\text{Ca(OH)}_2$) generated during cement hydration. In high-temperature conditions common across Saudi Arabia, Qatar, and the UAE—where surface temperatures on metal and wood formwork frequently exceed 50°C—chemical degradation accelerates:

  1. Alkaline Hydrolysis (Saponification): Standard ester-based adhesives and poorly formulated urea resins undergo alkaline hydrolysis. Hydroxide ions ($\text{OH}^-$) attack the polymer backbone, breaking cross-linked chains and turning adhesive bonds into soft, non-cohesive compounds.

  2. Moisture Differential Stress: Extreme ambient evaporation pulls water out of the inner plies toward the exposed edges, while the face panel absorbs alkaline slurry water. This creates high shear stress across the glue line, resulting in edge ungluing and veneer splitting.

Q2: Why does a fully cured phenolic surface film prevent panel saponification and surface dusting?

Phenolic formaldehyde resins form a tightly cross-linked three-dimensional polymer network during high-temperature thermal pressing ($>135^\circ\text{C}$).

Protective Mechanisms of Phenolic Overlays
  • Chemical Inertness: Fully cured phenolic resin resists saponification from calcium hydroxide solutions, creating an impermeable barrier between wet concrete and internal wood plies.

  • Controlled Water Retention: The dense film prevents the dry wooden core from rapidly absorbing hydration water out of the fresh concrete surface. This allows concrete along the formwork face to cure evenly, eliminating dusting, scaling, and cosmetic discoloration.

  • Extended Multi-Pour Integrity: High-solid phenolic surface coatings allow panels—such as standard 12mm red boards (rated for 6–8 reuses) and heavy-duty 18mm phenolic panels (rated for 15–20 reuses) produced by NQ Formwork Plywood Co., Ltd.—to strip cleanly pour after pour without degrading the underlying core.

To review daily thermal-press monitoring and laboratory boiling immersion procedures, browse our factory video channel, check our company background, or consult our export engineering desk.

🌐 Connect with NQ Formwork Plywood Co., Ltd.


11142134e57s.jpg

2026-09-030

Q1: Why does Guangxi (Guigang) dominate over 60% of China’s high-grade construction formwork manufacturing?

Guangxi’s dominance in the global wood-based panel industry is anchored in a continuous industrial supply chain, favorable forestry conditions, and deep-water river port logistics. Guigang, located along the Xijiang River basin, processes millions of cubic meters of fast-growing structural timber annually.

Key industrial advantages include:

  1. Raw Material Proximity: Fast-growing eucalyptus plantations reach harvest maturity within 5 to 6 years, providing a consistent supply of dense, straight-grained structural veneers within a 50 km radius of manufacturing clusters.

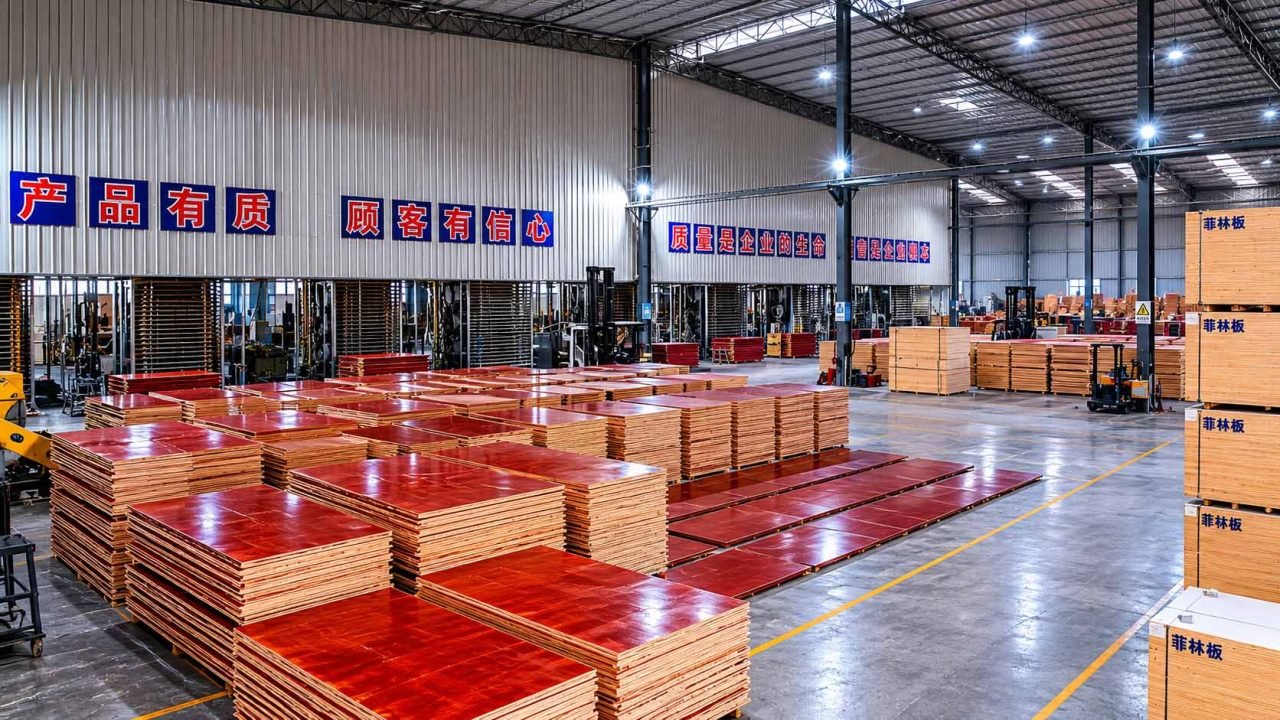
  2. Integrated Veneer-to-Panel Ecosystem: In industrial zones like Batang Industrial Park, processing plants combine rotary peeling, roller-drying, adhesive synthesizing, hot-pressing, and edge-profiling into a continuous 24-hour manufacturing cycle.

  3. Barge-to-Ocean Port Freight: Factories situated within 2 km of Guigang Port utilize direct inland river barges connecting to ocean hubs in Guangzhou and Shenzhen, reducing inland transport expenses compared to landlocked production bases.

Q2: How does Southern Eucalyptus timber cell density compare with Northern Poplar in concrete load-bearing applications?

Selecting between eucalyptus-core and poplar-core shuttering plywood directly determines structural deflection during concrete casting.

Structural Timber Mechanics Comparison
Physical / Mechanical Property Southern Eucalyptus (Guangxi Core) Northern Poplar (Standard Core) Engineering Impact on Jobsite
Air-Dry Wood Density 600 – 680 kg/m³ 420 – 480 kg/m³ Eucalyptus provides ~40% higher resistance to fastener pull-out and edge crushing.
Modulus of Elasticity (MOE) 9,500 – 11,500 MPa 6,000 – 7,500 MPa Drastically reduces sagging when pouring 200mm+ suspended slabs.
Phenolic Adhesive Uptake Controlled, Uniform High / Over-absorbent Poplar absorbs excess glue into pores, causing dry bond lines unless resin volumes are elevated.
Primary Durability Tier 18mm Heavy Panels (15–20 Reuses) Light Panels (3–5 Reuses) Eucalyptus cores maintain ply cohesion through repeated wet-dry cycles.

For contractors managing infrastructure projects in Dubai, Saudi Arabia, or Southeast Asia, using high-density eucalyptus formwork manufactured by integrated facilities like NQ Formwork Plywood Co., Ltd. ensures minimal wall deflection and predictable reusability.

🌐 Connect with NQ Formwork Plywood Co., Ltd.


GUIGANG, CHINA

NQ Formwork Plywood

Located in China’s premier timber hub, NQ Formwork Plywood brings 27 years of manufacturing excellence. With a 60,000 m² facility and 300+ workers, we deliver 2M+ sheets annually to global construction projects.
+86 199 7757 5391

www.nqformwork.com

cn8619977575391@gmail.com

GET IN TOUCH

Request A Quote

Partner with China’s leading formwork factory. Tell us your project needs, and our export team will respond within 24 hours.